Compare side-by-side engineering specifications, spindle torque, RPM, axis travels, tool capacity, CNC controllers, and digital telemetry standards for Mazak INTEGREX i-200H S vs Nakamura-Tome WT-150II.
|
Specification Matrix
Verified OEM & MachineSchema Data
|
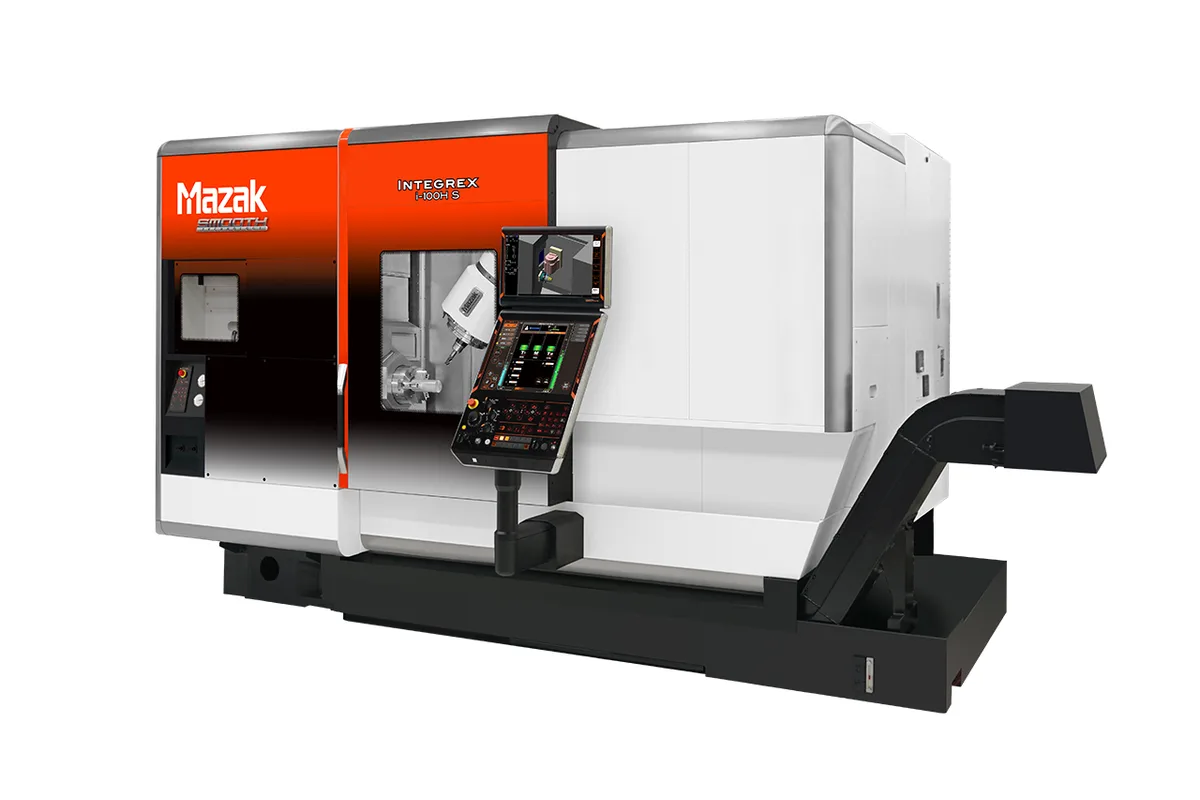
Mazak
View Specs Page →
|
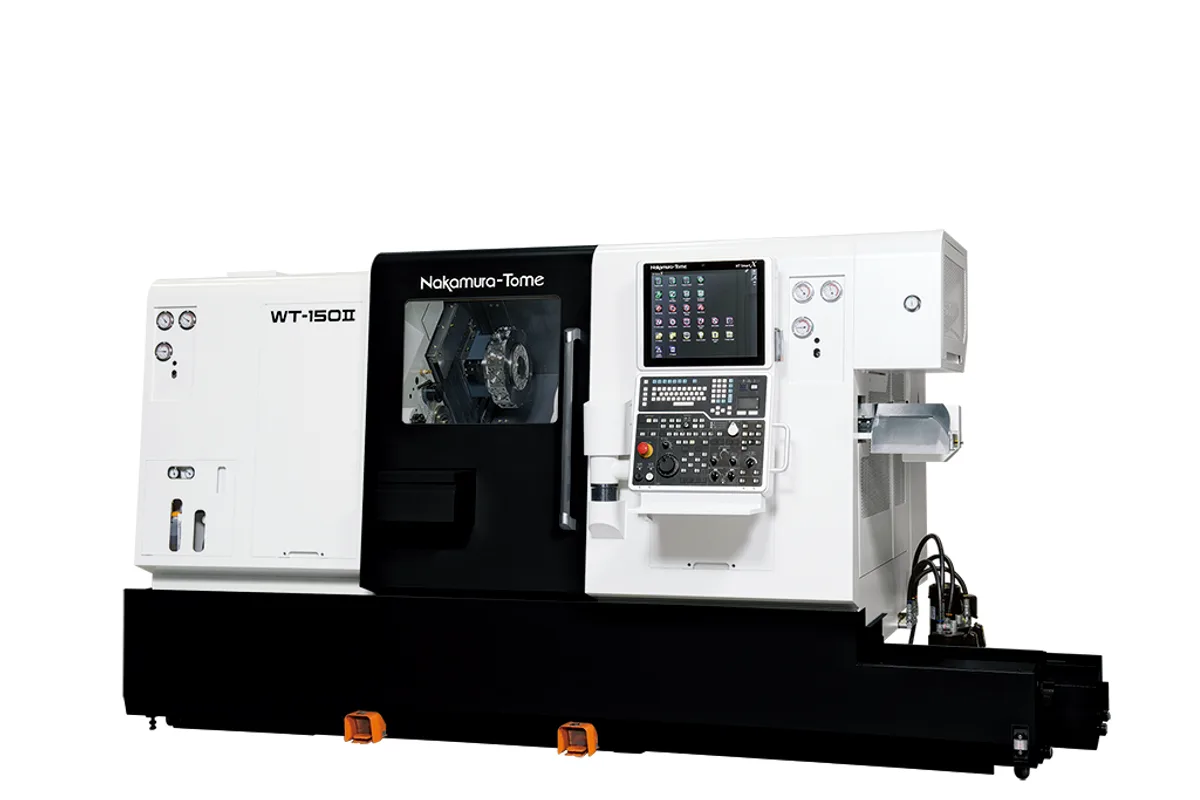
Nakamura-Tome
View Specs Page →
|
|---|---|---|
| 1. Machine Classification & Kinematics | ||
| Machine Type | Multi-Tasking & Mill-Turn Machines | Multi-Tasking & Mill-Turn Machines |
| Controlled Axes | 5-Axis Simultaneous | 8-Axis Simultaneous |
| OEM Headquarters | Japan | Japan |
| Model Status / Year | 2024 | 2024 |
| 2. Spindle Speed & Motor Power | ||
| Maximum Spindle Speed | 12,000 RPM Highest RPM | 5,000 RPM |
| Spindle Motor Rating | 22.0 kW (29.5 HP) More Power | 15.0 kW (20.1 HP) |
| 3. Work Envelope & Travels (X / Y / Z) | ||
| X-Axis Travel | 615 mm Longest X | 195 mm |
| Y-Axis Travel | 260 mm Longest Y | 70 mm |
| Z-Axis Travel | 1,077 mm Longest Z | 600 mm |
| Table Surface Dimensions | Standard Worktable | Standard Worktable |
| Maximum Table Payload | Standard Capacity | Standard Capacity |
| 4. Tool Changer (ATC) & Motion Rates | ||
| Tool Magazine Capacity | 72 Tools Largest ATC | 48 Tools |
| Rapid Traverse Rate | 40 m/min | 40 m/min |
| 5. CNC Control & Telemetry Standards | ||
| Standard CNC Controller | MAZATROL SmoothAi | NT-SmartX with Fanuc 31i-B |
| MTConnect Telemetry Standard | ANSI/MTC1.4 Verified | ANSI/MTC1.4 Verified |
| 6. Machine Mass & Rigidity | ||
| Net Machine Weight | 11,800 kg Heaviest Base | 8,500 kg |
When evaluating Mazak INTEGREX i-200H S vs Nakamura-Tome WT-150II, shop managers must weigh spindle kinematics against overall structural rigidity. The Mazak INTEGREX i-200H S delivers a competitive edge in heavier stock removal with its 22.0 kW spindle motor. Both builders adhere to standardized industrial communication protocols, facilitating MTConnect machine monitoring across digital factory floors.
When selecting between competing machining centers or turning centers, specification sheets provide only the baseline. Experienced manufacturing engineers should analyze the following core metrics:
Check whether kW and torque are rated continuously or at 15-30 minute duty cycles for roughing operations.
Heavier meehanite cast-iron machine beds absorb cutting harmonics and damp vibrations during high-feed milling.
Ensure the control system supports high-speed look-ahead (G05.1/G08) and standard MTConnect IoT monitoring.